Can Natural Pigments Survive PLA and PBS Extrusion?
Natural pigments can color PLA and PBS, but thermal stability and lightfastness remain key challenges during processing and use.
Color plays an important role in the appearance of plastic products, but conventional pigments can conflict with sustainability objectives. As biodegradable polymer use increases, researchers are examining whether natural colorants can withstand industrial melt processing while maintaining color, flow behavior, and mechanical performance.
The study Sustainability in the Development of Natural Pigment-Based Colour Masterbatches and Their Application in Biopolymers examined this question using four commercial natural pigments: blue spirulina, yellow curcumin, red beetroot, and green chlorophyllin. The researchers combined the pigments with polylactic acid (PLA) and polybutylene succinate (PBS) to produce color masterbatches through twin-screw extrusion. They then diluted the masterbatches into the corresponding polymer matrices at 2, 4, and 6 wt% and produced test specimens by injection molding. The masterbatch formulation also included titanium dioxide, calcium carbonate, and stearic acid to support UV protection, dispersion, and processing.
You can also read: Recycled Cobalt Pigment Adds Color and Flame Retardancy to PLA
Heat Creates the First Challenge
Heat presents one of the main processing challenges for natural pigments. Their organic structures can begin to degrade at lower temperatures than the polymers they are added to. Thermogravimetric analysis identified degradation onset temperatures of approximately 229 °C for spirulina, 244 °C for curcumin, 258 °C for chlorophyllin, and 267 °C for beetroot. PLA and PBS showed considerably higher degradation temperatures.
The researchers therefore selected extrusion temperature profiles that allowed each polymer to melt while limiting thermal exposure of the pigments. Processing temperatures reached 145 °C for PBS and 190 °C for PLA. The twin-screw extruder operated at 65 rpm with a feed rate of 2 kg/h.
The selected processing window suited most pigment–polymer combinations, though spirulina remained a notable exception. During PLA processing, spirulina lost its characteristic blue color, preventing the production of a blue PLA masterbatch. PBS’s lower processing temperature preserved sufficient pigment stability for successful compounding. This result shows that pigment compatibility depends strongly on the polymer matrix’s thermal processing requirements.
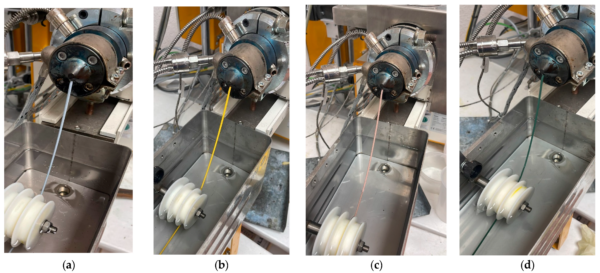
Twin-screw extrusion of PBS-based masterbatches containing natural pigments: (a) spirulina, (b) curcumin, (c) beetroot, and (d) chlorophyllin. The different strand colors illustrate pigment retention during melt processing. Courtesy of Sustainability in the Development of Natural Pigment-Based Colour Masterbatches and Their Application in Biopolymers.
Flow Behavior Remains Manageable
From a processing perspective, the natural pigments caused only limited changes in the polymer matrix’s rheological behavior. Melt flow rate decreased slightly after pigment incorporation, indicating a modest increase in melt viscosity. Neat PLA showed an MFR of about 50 g/10 min, while the corresponding natural-pigment masterbatches stayed close to that value. PBS showed a similar response, with only a minor reduction in melt flow rate.
For compounders, that result matters. A natural color system offers little practical value if it forces major changes to screw design, pressure settings, or molding conditions. In this study, conventional twin-screw compounding and injection molding handled most formulations without major processing problems.
Color Without a Mechanical Penalty
The researchers also checked whether the masterbatches changed tensile and impact behavior. Across the 2 to 6 wt% addition range, neither PLA nor PBS showed significant losses in overall mechanical performance.
PLA started with a Young’s modulus of about 1710 MPa and tensile strength of 65.6 MPa. PBS started at about 392 MPa and 34.5 MPa, respectively. The colored formulations stayed close to those baselines. Impact strength also remained within a similar range, although individual pigments produced some variation.
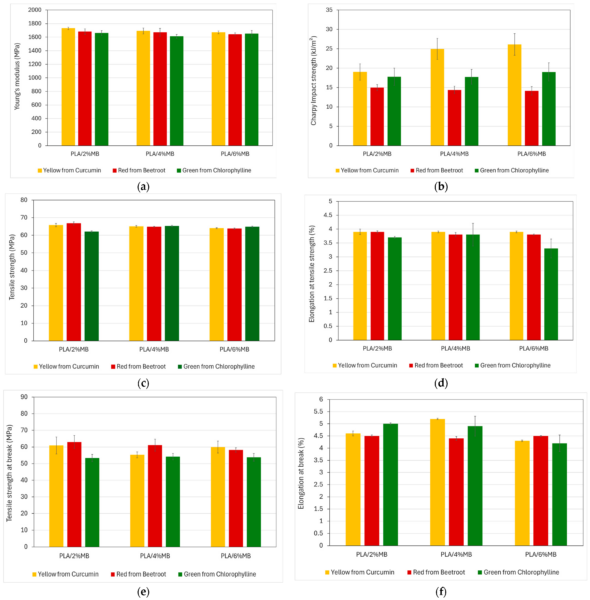
Mechanical properties of PLA containing 2, 4, and 6 wt% masterbatches based on curcumin, beetroot, and chlorophyllin pigments. Courtesy of Sustainability in the Development of Natural Pigment-Based Colour Masterbatches and Their Application in Biopolymers.
Light Stability Exposes the Weak Point
Successful extrusion did not ensure long-term color stability. After 50 hours of Xenon-lamp exposure, most formulations showed a color difference above ΔE* = 2, indicating a visually perceptible change. The PLA formulation containing 2 wt% green chlorophyllin masterbatch showed the highest photostability and remained the main exception.
The study therefore points to UV stability as the largest barrier to broader use. Packaging, consumer products, agricultural parts, and outdoor applications may require additional stabilization, protective coatings, or pigment modification before natural colors can compete with conventional systems over long service periods.
A More Sustainable Route to Color
The environmental comparison also favored the natural pigments. Under the study’s assumptions, one kilogram of curcumin pigment generated about 0.04 kg CO2-eq, compared with 18.65 kg CO2-eq for the inorganic green reference pigment. Their natural-pigment masterbatches also consumed less electricity during extrusion and pelletizing.
Natural pigment masterbatches still require further development, particularly in lightfastness and thermal stability. Nevertheless, the study demonstrates that several natural colorants can be compounded into PLA and PBS using conventional processing equipment, with only limited changes in melt viscosity and mechanical performance. Future development should focus on improving color stability during processing and subsequent service exposure.
María José Vargas is a mechanical engineer and MSc candidate in Materials Engineering and Nanotechnology at Politecnico di Milano. Her work focuses on environmental stress cracking in polyethylene, polymer failure behavior, plastics processing, and sustainable polymer applications.